
Сипаттама
Hangzhou Ever-Power Sprocket Co., Ltd.
In a dairy plant, the conveyor runs during production and the CIP system runs during cleaning. Neither stops for the other. The sprocket has to survive both — every single day.
The Dairy CIP Cycle and What It Does to a Standard Sprocket
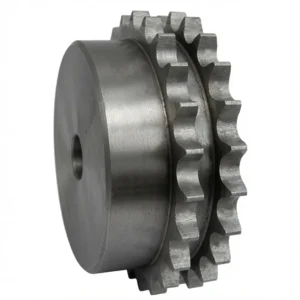
Clean-in-place (CIP) in a dairy facility typically runs two or three times daily: a hot caustic wash (NaOH, 70–80 °C) to break down protein and fat, followed by a hot acid wash (HNO₃ or citric acid) to remove mineral deposits, followed by a hot water rinse and sometimes a sanitising dose. For a carbon steel sprocket mounted near a conveyor belt that passes through these zones, this cycle is lethal. The alkaline wash strips surface oxides, the acid wash attacks the exposed bare metal, and the repeated thermal cycling between hot cleaning and ambient production temperatures accelerates scale formation and corrosion under any residual deposit. Within 6–12 weeks, tooth flanks that started at a clean machined finish are carrying rust scale that transfers to the chain and introduces contamination risk to the dairy product stream. The Ever-Power #35 тот баспайтын болаттан жасалған жұлдызша in 316 SS is engineered around this exact duty cycle. The passive oxide layer regenerates after each acid wash. No scale forms. No rust transfers. The cleaning cycle that destroys carbon steel is simply part of the operating environment, not a threat to the component.
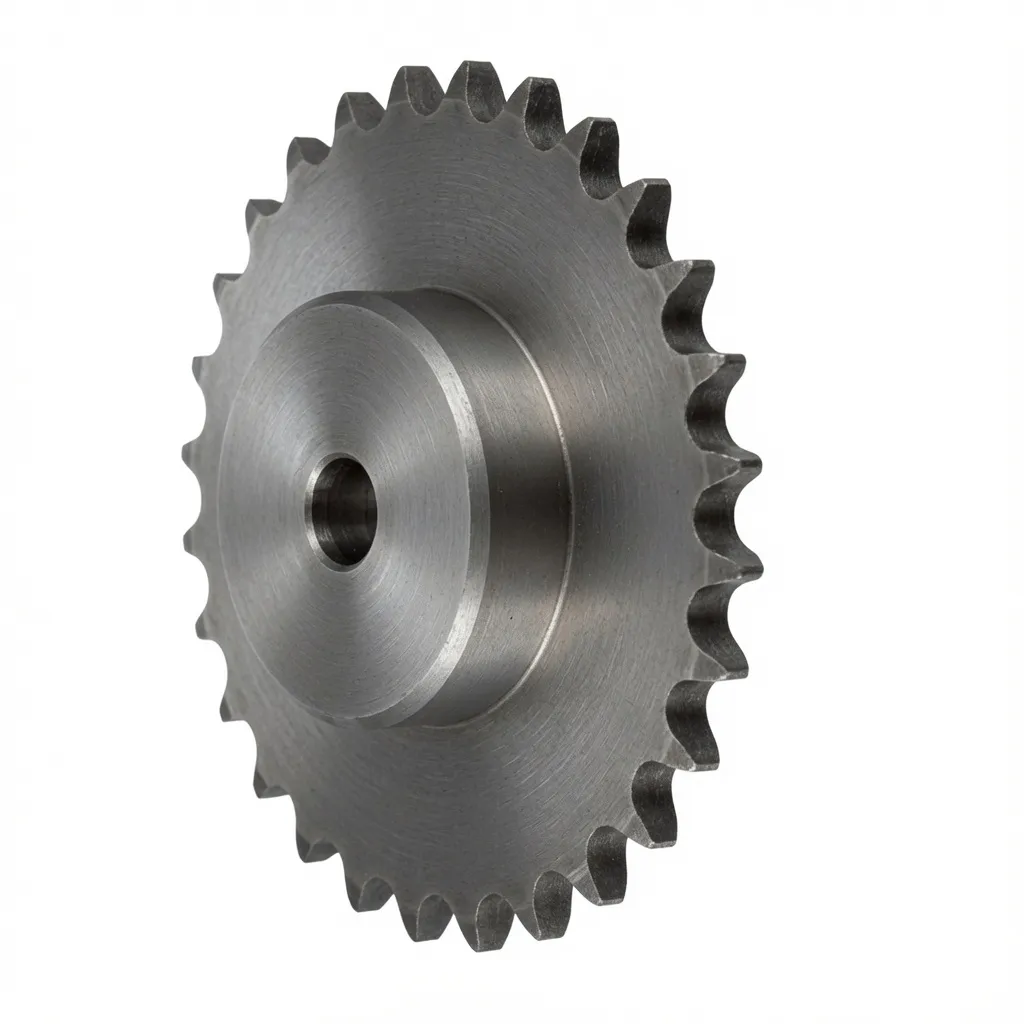
Why 316 SS and Not 304 for Dairy Lines
Both 304 and 316 SS resist NaOH caustic washing well. The difference emerges in the acid wash stage. Nitric acid (HNO₃) used in dairy CIP is actually passivating for both grades — it removes free iron and thickens the oxide layer, making it beneficial. But nitric acid at higher concentrations or temperatures, combined with any residual chloride from water hardness or residual sanitiser, can pit 304 SS over time. Grade 316, with its 2–3% molybdenum addition, resists this chloride-assisted pitting reliably through years of daily acid cycles. The practical recommendation for dairy lines running HNO₃ or peracetic acid CIP is straightforward: specify 316 SS for all conveyor drive components and eliminate the corrosion variable from your maintenance planning entirely.
Техникалық сипаттамалар
| Параметр | Құндылық |
|---|---|
| Тізбек нөмірі | ANSI 35 |
| Ұсыныс | 9,525 мм (3/8 дюйм) |
| Материал | 304 SS / 316 SS (316 recommended for CIP) |
| Тіс диапазоны | 6T – 60T |
| Ұңғыма төзімділігі | H7 стандарты |
| Сәйкестік | ANSI B29.1, ISO 9001:2015 |
Maintenance Planning Around Stainless: What Changes
Dairy maintenance teams that switch from carbon steel to 316 SS sprockets typically report one immediate practical change: sprocket condition stops being a limiting factor in the planned maintenance schedule. Instead of replacing sprockets at each planned shutdown because they are certain to be corroded regardless of mechanical wear, the team can inspect and assess — and in most cases, the SS sprocket passes inspection and stays in service for another cycle. This shifts maintenance resources to chain inspection (which still has a wear-based replacement cycle) and away from a corrosion-driven sprocket replacement that was consuming parts budget and wrench time without any mechanical justification.
Companion Parts for a Complete CIP-Resistant Drive
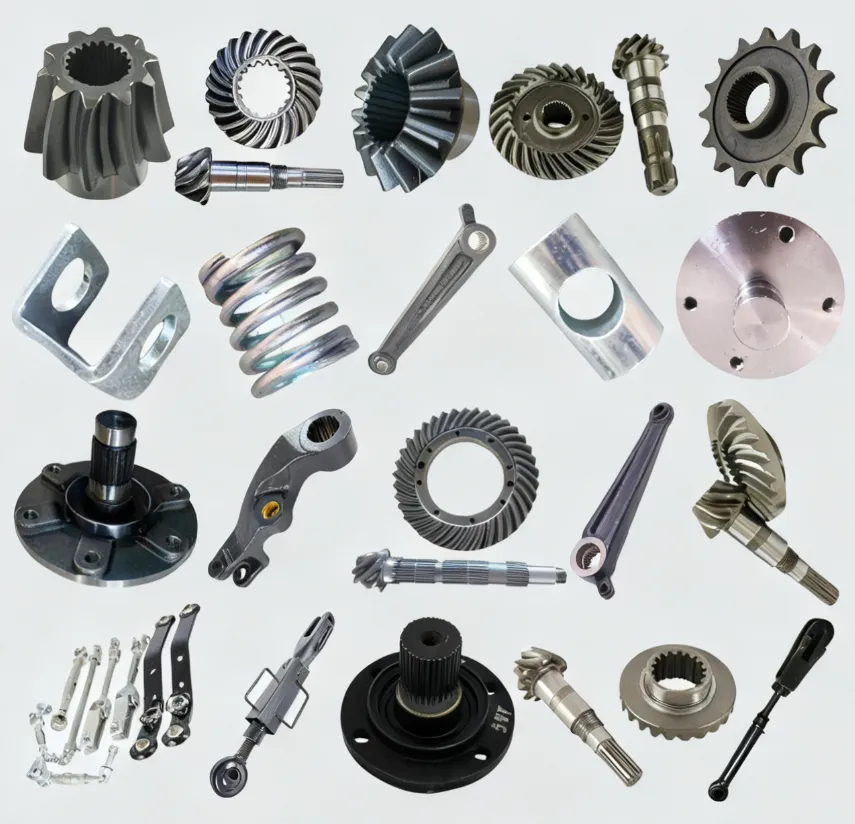
A fully CIP-resistant drive pairs the тот баспайтын болаттан жасалған жұлдызша with same-grade chain and hardware throughout. We supply the complete set:
- ANSI 35 SS роликті тізбегі — 316 grade, matched to sprocket material
- NSF H1 Drip Lubricator — food-grade oil system for enclosed dairy conveyor drives
- SS Spring-Clip Master сілтемелері — easy chain removal for strip-down cleaning
- Конус тәрізді құлыптаулы бұталар жиынтығы — for rapid sprocket removal without shaft dismantling
- SS Idler жұлдызшалары — for tensioning and slack-side guidance
What Dairy Maintenance Teams Report
“We run triple-daily CIP on our pasteurisation conveyor. Previous carbon sprockets needed replacing at every 6-week shutdown. The 316 SS Ever-Power units went 18 months before the first tooth wear measurement — and the measurement was within tolerance.”
“Switched our cheese-cutting conveyor drive entirely to Ever-Power 316 SS — sprockets, chain, and idlers. The uniform material grade made our food-safety audit straightforward. No mixed materials to explain.”
“Good quality and correct H7 bore on the first order. We appreciated that passivation was included without being asked. Lead time for the custom tooth count was 12 days — acceptable for planned maintenance.”
Ready to Eliminate Corrosion from Your Maintenance Schedule?
+86-571-88220653 | [email protected] | Шэньхуа жолы, Ханчжоу, Қытай
Толық ақпаратты шолыңыз тот баспайтын болаттан жасалған жұлдызшалар жиынтығы немесе келіңіз Біз туралы бет.


Пікірлер
Әзірге ешқандай пікір жоқ.