
Description
Hangzhou Ever-Power Sprocket Co., Ltd.
At the #100 pitch, a material defect inside the sprocket body is not a quality issue — it is a safety incident waiting to happen. We test for it before the first cut is made.
Why Material Integrity Testing Comes Before Machining
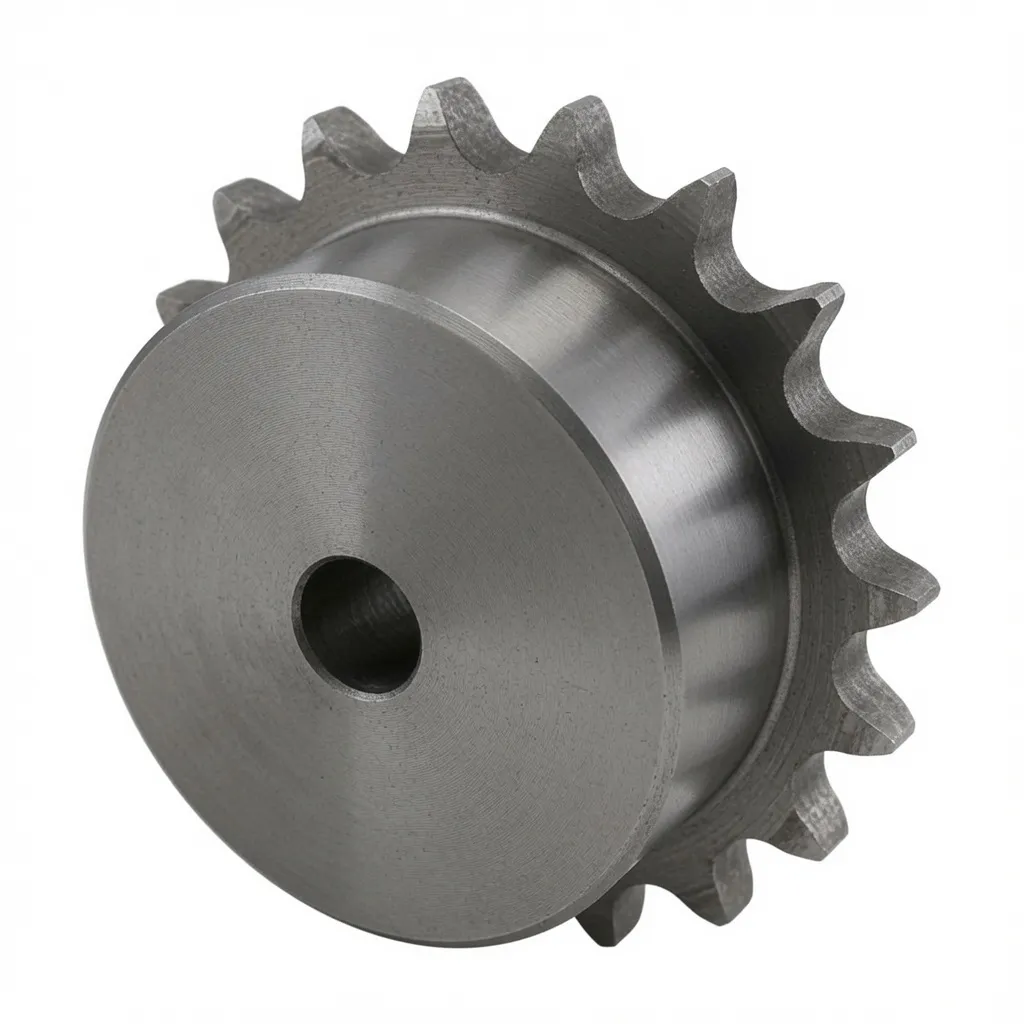
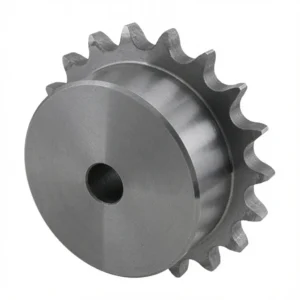
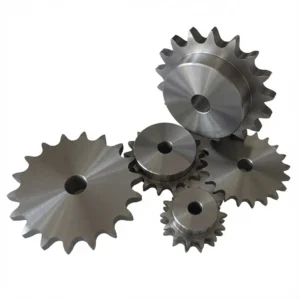
At the #40 or #50 pitch scale, an internal void or lamination in the stainless billet might never affect performance — the cross-sections are small enough and load paths redundant enough that a subsurface defect in an off-load zone has little practical consequence. At the #100 pitch, with 31.75 mm chain and roller loads that can exceed 20 kN per tooth in heavy-duty applications, this calculation changes fundamentally. A lamination at the tooth root cross-section can initiate fatigue cracking under cyclic load without any visible surface indication, producing sudden tooth fracture that jams a conveyor, damages downstream equipment, or — in the worst case on an overhead drive — causes an uncontrolled load drop. This is why our Ever-Power #100 Stainless Steel Sprocket production starts with billet inspection, not machine setup. Every bar over 120 mm diameter is ultrasonically tested per ASTM A388 before a single cut is taken. Only UT-cleared material progresses to the shop floor.
PMI Testing and Full Material Traceability
Positive material identification (PMI) is a rapid XRF scan that confirms the elemental composition of each billet against the declared grade. It takes under 60 seconds per piece and eliminates the risk of grade substitution — an issue more common than most buyers realise in the SS long-products market, where 304 and 316 bars look identical and the grade difference is detectable only by chemistry. Our PMI protocol tests every individual billet, not just a sample from each delivery lot. The test record, along with the mill certificate and UT clearance, is retained against the billet heat number and cross-referenced to the finished sprocket serial number on the production traveller document that ships with each order. That chain of traceability — from raw bar to boxed sprocket — is the documentation that satisfies the most stringent OEM quality audits.
Solution Annealing for Maximum Corrosion Resistance
After rough machining, the #100 SS sprocket blanks undergo solution annealing: heating to 1,050–1,100 °C followed by rapid water quench. This dissolves any chromium carbide that may have precipitated during hot-working of the original billet, producing a fully homogenous austenitic microstructure with maximum chromium in solid solution — and therefore maximum corrosion resistance throughout the cross-section. This treatment is standard on all our #100 SS sprockets and is documented on the production traveller.
Technical Specifications
| Parameter | Value |
|---|---|
| Chain No. | ANSI 100 |
| Pitch | 31.75 mm (1-1/4″) |
| Roller Diameter | 19.05 mm |
| Material | 304 SS / 316 SS (PMI tested) |
| Billet QC | UT per ASTM A388 + PMI per item |
| Heat Treatment | Solution anneal 1,050–1,100 °C + water quench |
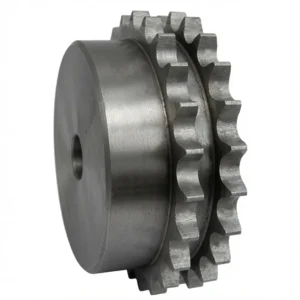
| Tooth Range | 8T – 48T (larger on request) |
| Compliance | ANSI B29.1 Class A, ASTM A388, ISO 9001:2015 |
Applications Where #100 SS Is the Only Viable Answer
| Industry | Machine | Critical Factor |
|---|---|---|
| Steel Mill | Scale-breaker conveyor, pickling line | HCl acid mist + high load |
| Continuous Casting | Strand guide withdrawal chain | Thermal cycling + steam |
| Offshore Platform | Mooring tensioner, crane drive | Seawater + shock load |
| Heavy Chemical | Reactor charging conveyor | Acid / alkali exposure + mass load |
Heavy-Duty Drive System Components
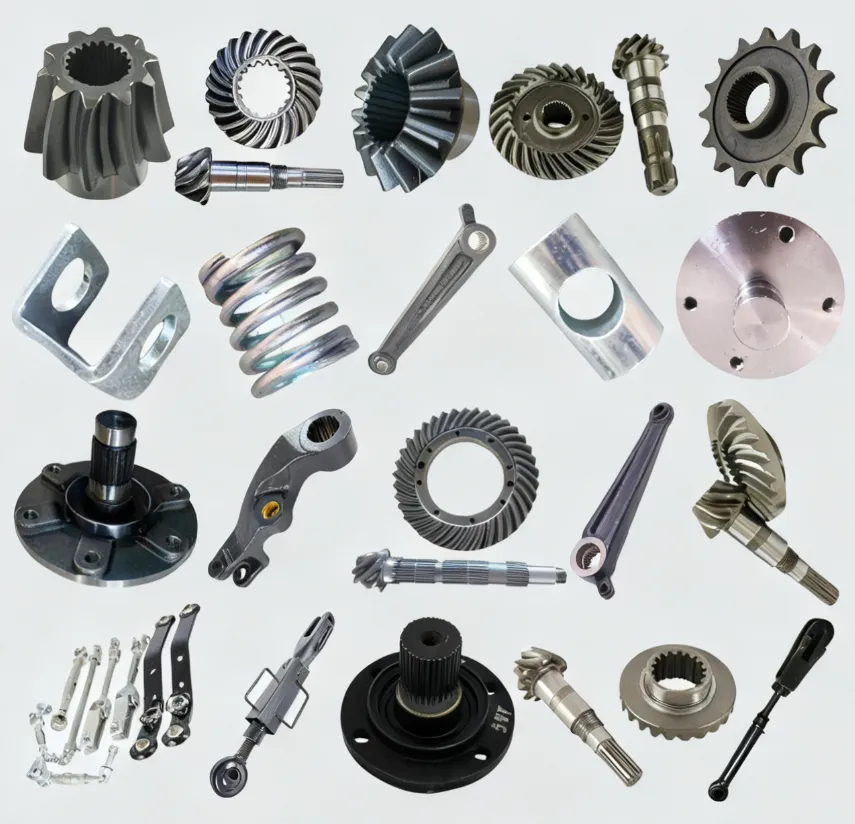
- ANSI 100 SS Roller Chain — 316 SS, single and duplex strand
- 100H Heavy Series SS Chain — extra-thick outer plates for shock and overload
- Large QD Taper Bushings — SDS 4040–5050 series, stainless versions available
- Custom 316 SS Shafts — turned with keyways and locking collars
- Sprocket Alignment Tools — laser-alignment kits for precise chain-line setup
Customer Testimonials
“24 custom #100 SS sprockets for our acid pickling line. All arrived with UT clearance certs and CMM reports. Bore accuracy verified in-house — spot-on. The UT and PMI documentation satisfied our TÜV audit without question.”
“Mooring chain tensioner on an offshore platform — 316 SS #100 sprockets, 18 months of direct saltwater spray. Look brand new. The investment in 316 grade was the right decision.”
“Complex custom order with step-hub profile — drawings reviewed twice before machining, which we appreciated. Delivered in 22 days, reasonable for bespoke large stainless work.”
Enquire About UT-Tested #100 SS Sprockets
+86-571-88220653 | [email protected] | SHENHUA ROAD, HANGZHOU, CHINA
Explore the full stainless steel sprocket range or learn about our company on the About Us page.


Reviews
There are no reviews yet.